High-Precision Medical Furniture & Ward Solutions
Direct Factory Supply: CE & ISO Certified Medical Beds, Storage Systems, and Clinical Cabinets Manufactured to Strict International Standards.
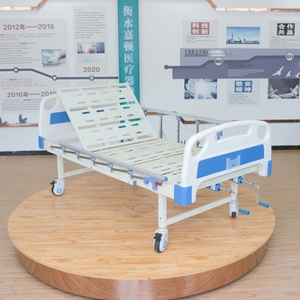
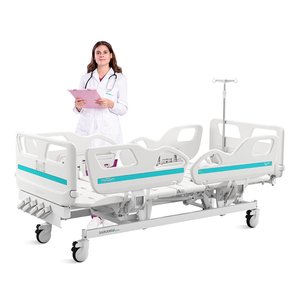
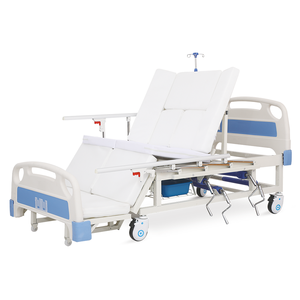
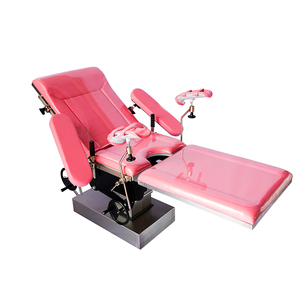
Global Export Authority & Manufacturing Benchmark
Empowering hospitals, critical care units, and medical distributors across 77+ countries with OEM/ODM production mastery.
1. Strategic Landscape of Medical Cabinet Manufacturing & Global Sourcing
In modern hospital architecture and clinical ward engineering, medical cabinets and specialized hospital furniture form the operational backbone of patient care management, infection control, and pharmaceutical logistics. As global healthcare infrastructure expands rapidly across North America, Europe, the Middle East, and Asia-Pacific, procurement directors are increasingly turning to leading China medical cabinet factories and OEM exporters to achieve an optimal balance between stringent international quality standards (such as CE, ISO 13485, ISO 9001, and EN 60601) and cost efficiency.
China's medical equipment manufacturing ecosystem has undergone a profound technological transformation over the past decade. Moving beyond standard sheet metal fabrication, top-tier Chinese manufacturers now integrate high-precision CNC fiber laser cutting, automated robotic arm welding, multi-stage nano-ceramic anti-corrosion pre-treatment, and automated electrostatic antimicrobial powder coating lines. This industrial elevation ensures that medical stainless steel medicine cabinets, ICU bedside lockers, narcotic storage safes, instrument trolleys, and nursing workstation cabinets meet the rigorous demands of sterile hospital environments.
Key Sourcing Drivers for Hospital Procurement Officers:
- Material Integrity & Structural Standards: Utilization of high-grade SUS 304/316 stainless steel and electro-galvanized cold-rolled steel (thickness ranging from 1.0mm to 1.5mm) to withstand aggressive chemical disinfection and prevent surface oxidation.
- Infection Prevention (HAIs Mitigation): Integration of silver-ion (Ag+) antimicrobial powder coatings that actively suppress bacterial growth (such as MRSA and E. coli) on cabinet handles, drawers, and contact surfaces by over 99.9%.
- Ergonomic & Modular Versatility: Modular internal tray architectures following ISO 6040 standards, allowing flexible configuration of medicine baskets, dividers, and telescopic full-extension slide rails.
- Regulatory Compliance & Export Readiness: Seamless compliance with EU Medical Device Regulation (MDR 2017/745), FDA registration, and rigorous third-party salt-spray corrosion testing exceeding 1,000 hours.
Core Factory Competencies & Quality Pillars
Why Tier-1 global hospital groups and government health ministries partner with our production facilities.
25+ Years Industrial Heritage
Decades of specialized R&D in medical furniture manufacturing, producing over 10,000 units annually for critical care units, maternity wards, emergency rooms, and outpatient clinics globally.
Certified Compliance (CE & ISO)
Full adherence to ISO 13485 medical device quality management, ISO 9001, and CE certifications. All products undergo rigorous mechanical load-bearing, stability, and surface resistance audits.
Global Logistics Footprint
Established supply chain channels exporting to 77+ countries worldwide with custom knock-down (KD) packaging or fully assembled shipping to minimize transit damages and freight tariffs.
2. Technical Specification & Material Standard Matrix
Selecting the correct material specification is vital to preventing premature equipment degradation, hospital-acquired infections (HAIs), and high maintenance costs. Below is an authoritative technical comparison matrix evaluated across three primary hospital cabinet categories:
| Feature / Technical Benchmark | Cleanroom & Surgical Cabinets | Ward & Bedside Storage Cabinets | Smart Pharmacy & Narcotic Safes |
|---|---|---|---|
| Primary Raw Material | SUS 304 / SUS 316 Stainless Steel | Electro-Galvanized Cold-Rolled Steel | Double-Walled Heavy Cold-Rolled Steel |
| Surface Treatment | Electropolished / Satin Finish | Antimicrobial Epoxy Powder Coating | Anti-Static Thermosetting Powder |
| Sheet Thickness Range | 1.2 mm - 1.5 mm Seamless Sheet | 1.0 mm - 1.2 mm Reinforced Frame | 1.5 mm - 2.5 mm Armor Grade |
| Infection Control Grade | Class 100 / ISO 5 Cleanroom | General Ward Antimicrobial | Controlled Environment Standard |
| Access & Lock Mechanism | Hermetic Touchless / D-Handle | Central Keyed / Soft-Close Latch | Biometric / RFID / Dual PIN Code |
| Corrosion Resistance | Salt Spray Test > 1,500 Hours | Salt Spray Test > 800 Hours | Salt Spray Test > 1,000 Hours |
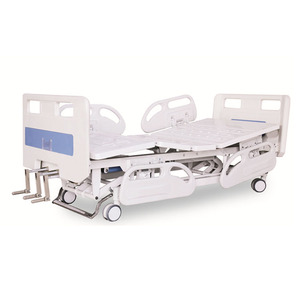
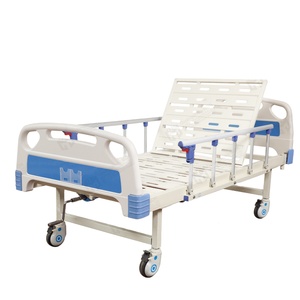
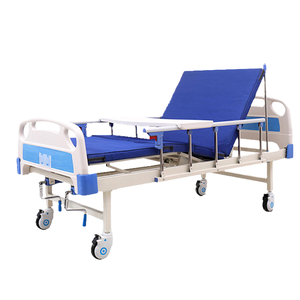
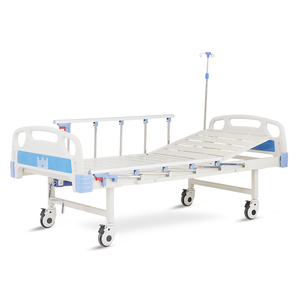
This technical standardization guarantees that whether a healthcare institution requires a simple 1-crank patient nursing bed or a complex stainless steel surgical instrument cabinet, structural integrity and biological safety remain completely uncompromised.
3. Future Procurement & Technological Trends in Hospital Storage (2025–2030)
As smart hospitals (Hospital 4.0) evolve, hospital furniture is transitioning from passive storage elements into intelligent, connected clinical assets. Procurement leaders must anticipate the following key trends when negotiating supply contracts with OEM factories:
A. Integration of RFID & Real-Time Inventory Tracking (RTLS)
Modern pharmaceutical cabinets and high-value medical device storage units are increasingly embedded with UHF RFID sensors and automated weight scales. When a nurse removes a surgical suture or controlled medication, the cabinet automatically logs the transaction into the Hospital Information System (HIS) and Electronic Health Record (EHR) software, preventing stockouts and reducing manual auditing labor by over 70%.
B. Modular ISO 6040 Standardization & Rapid Ward Reconfiguration
Disaster preparedness and fluctuating patient admission rates require medical cabinets that offer modular adaptability. The adoption of standardized ISO 6040 tray systems allows nurses to swap entire drug trays from central storage to mobile crash carts or ward medicine cabinets without transferring individual vials, significantly reducing medication dispensation errors.
C. Environmental Sustainability & Green Hospital Initiatives
With global healthcare organizations committing to Net-Zero carbon footprints, Chinese exporters are adopting eco-friendly manufacturing methods. This includes volatile organic compound (VOC)-free powder coatings, 100% recyclable stainless steel alloys, solar-powered factory operations, and optimized flat-pack shipping packaging that increases container volume efficiency by up to 40%.
D. Enhanced Ergonomics & Noise Mitigation in Critical Wards
Hospital sleep hygiene is directly tied to patient recovery times. Future medical cabinet designs prioritize soft-close hydraulic hinges, silent TPU double-wheel casters, and dampened drawer slides that keep operational noise below 35 decibels (dB), creating a serene environment in intensive care units (ICUs) and pediatric wards.
Frequently Asked Questions for Global Procurement Officers
Direct answers regarding MOQ, custom OEM/ODM capabilities, international logistics, and quality assurance.
Ready to Partner with China's Premier Medical Cabinet Manufacturer?
Get direct factory price quotes, technical CAD drawings, and comprehensive product catalogs tailored for your hospital project or distribution network within 24 hours.
Send an Inquiry